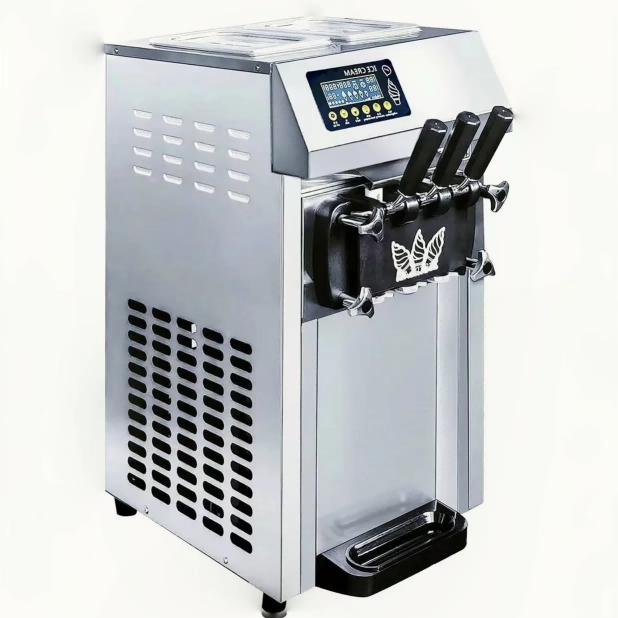
Professional Table Top Soft Serve Ice Cream Machine: Commercial Grade Performance in a Compact Design

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

table top soft serve ice cream machine

The table top soft serve ice cream machine represents a revolutionary advancement in compact ice cream production technology. This versatile unit combines professional-grade performance with space-saving design, making it ideal for various food service establishments. The machine features precision temperature controls that maintain optimal consistency, while its user-friendly interface allows operators to adjust settings easily. Advanced refrigeration systems ensure rapid freezing and maintain proper product temperature throughout service hours. The unit typically accommodates multiple flavor options and includes separate hoppers for mix storage. Built with commercial-grade stainless steel components, these machines offer durability and easy cleaning protocols. Most models feature automatic standby modes to preserve energy during low-traffic periods and integrated safety systems to protect both operators and product quality. The mechanical components include heavy-duty compressors and efficient freezing cylinders that deliver consistently smooth product texture. With production capabilities ranging from 20-30 servings per hour, these machines meet the demands of small to medium-sized operations while maintaining product quality and operational efficiency.

New Products

Table top soft serve ice cream machines offer numerous practical benefits that make them an excellent investment for food service businesses. First, their compact design maximizes counter space utilization while delivering professional-quality results, perfect for establishments with limited space. The machines' automated operation significantly reduces labor costs and ensures consistent product quality with minimal staff training required. Energy efficiency features, including standby modes and smart power management, help control operational costs while maintaining product readiness. The versatility of these units allows for quick flavor changes and the ability to serve various frozen desserts, from traditional ice cream to frozen yogurt and sorbet. Maintenance is straightforward, with easily accessible components and simple cleaning procedures that comply with health regulations. The machines' reliable performance and durable construction minimize downtime and repair costs, ensuring a better return on investment. Advanced temperature monitoring systems prevent product waste by maintaining optimal serving conditions throughout operating hours. The ability to adjust overrun levels allows operators to customize product consistency and maximize profitability. These machines also feature user-friendly controls that simplify operation and reduce the likelihood of errors. The integrated safety features protect both operators and the equipment, extending the machine's service life while ensuring safe operation.

Latest News

Baratza Encore ESP: The Coffee Grinder That Changes Your Coffee Game

20

May

Baratza Encore ESP: The Coffee Grinder That Changes Your Coffee Game

View More
Top 5 Best Coffee Grinders for Perfectly Ground Beans

20

May

Top 5 Best Coffee Grinders for Perfectly Ground Beans

View More
Blender Market: The Ultimate Resource for 3D Creators.

06

Jun

Blender Market: The Ultimate Resource for 3D Creators.

View More
Best Blender Market Add-Ons for Efficient 3D Workflows.

06

Jun

Best Blender Market Add-Ons for Efficient 3D Workflows.

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

table top soft serve ice cream machine

Advanced Temperature Control System

Advanced Temperature Control System

The sophisticated temperature control system in table top soft serve ice cream machines represents a significant technological advancement in frozen dessert preparation. This system maintains precise temperature levels throughout the freezing process, ensuring consistent product quality from the first serve to the last. The technology incorporates multiple temperature sensors strategically placed throughout the machine, continuously monitoring and adjusting conditions in real-time. This level of control prevents ice crystal formation and maintains the ideal serving consistency. The system also features smart adaptation capabilities, automatically adjusting to ambient temperature changes and usage patterns to maintain optimal performance. This precise control not only ensures product quality but also contributes to energy efficiency and reduced operational costs.
Multi-Flavor Capability with Independent Controls

Multi-Flavor Capability with Independent Controls

The multi-flavor functionality of modern table top soft serve machines revolutionizes menu offerings and operational flexibility. Each flavor hopper operates independently, allowing operators to serve different products simultaneously without flavor cross-contamination. The system includes separate temperature controls for each hopper, ensuring optimal serving conditions for different product types. This feature enables businesses to offer a diverse menu while maintaining consistent quality across all flavors. The independent control system also allows for easy flavor rotation and product experimentation, helping businesses adapt to changing customer preferences and seasonal demands. Advanced mixing technology ensures proper product incorporation and consistent flavor distribution throughout service.
Smart Digital Interface and Monitoring

Smart Digital Interface and Monitoring

The intelligent digital interface represents the cutting edge of soft serve machine technology, offering unprecedented control and monitoring capabilities. The system provides real-time feedback on machine performance, product temperature, and usage patterns through an intuitive touchscreen display. This interface allows operators to easily adjust settings, monitor maintenance needs, and track product usage. Built-in diagnostic tools help identify potential issues before they become problems, reducing downtime and maintenance costs. The system can store multiple product recipes and settings, ensuring consistency across different operators and shifts. Advanced monitoring features include automatic alerts for low mix levels, temperature variations, and required maintenance, helping maintain optimal operation and product quality.